One-sentence conclusion: this wave of order shifting gets stuck first at the drawing review stage
Whether you can take on high-end precision part orders is judged not by how many five-axis machines are listed in the equipment list, but by whether you have understood the drawing and marked the uncertain items before quoting. A quote with inadequate drawing review is essentially an uncertain bet—betting that thin walls will not deform, betting that the tool for a deep cavity is long enough, betting that no one will take that roughness note seriously. If you lose the bet, lead time, rework, and inspection criteria all have to be renegotiated.
This rule has boundaries for when it holds. When drawing information is complete, materials are conventional, batch size is stable, and tolerance annotations match function, quoting directly is more efficient, and clarifying item by item instead slows the pace. The scenarios where it fails are very concentrated: wall thickness below about 0.8 mm, features smaller than about 2.5 mm, a relatively large depth-to-width ratio for deep cavities, tight tolerances mixed with non-functional surfaces, and missing or vague annotations—in these cases, clarify first and then quote, and what you save is the rework cost of the entire downstream chain.
This becomes clearer when placed in the industry context. According to publicly available industry report figures (Zhiyan Consulting, China Commercial Intelligence Network, 2024–2025), the global precision parts manufacturing market is on the order of about USD 180–200 billion; China's precision instrument market was about RMB 898.8 billion in 2024 and is forecast at about RMB 943.74 billion in 2025; consumer electronics precision structural parts and modules are on the order of about USD 66–70 billion, of which smartphone applications account for about 64%. These are statistical and forecast figures under the reports' definitions, not any factory's capacity commitment. What they show is this: order volume exists, but orders are shifting from looking only at unit price to looking at verifiable engineering capability—and the first gate of engineering capability is drawing review.
Below, we proceed in the rhythm of "annotation—consequence—fix" and break it down category by category. Let's start with the least conspicuous but most expensive type of annotation.
The most expensive thing in a drawing is often not a dimension, but that note
When a price difference appears on a quote, procurement's first reaction is "this supplier is expensive." But if you break down two quotes, the main dimension tolerances are exactly the same; what differs is that line in the title block, "deburr and blunt all sharp edges," or the "Ra0.4" written next to a mating surface. These two lines do not change part function, yet they directly change the number of setups, toolpaths, manual finishing labor, and inspection items. A common situation in the industry is this: for the same drawing, different interpretations of the annotations can produce a one-tier difference in quote, and lead time changes accordingly. So the first step in drawing review is not measuring dimensions, but reading the annotations one by one and asking, "To what extent does this line actually require?"
How an annotation turns from a line of text into a cost item
"Blunt and deburr" sounds harmless, but in machining it depends on the case: if it only means removing hand-catching burrs, an ordinary deburring tool or vibratory finishing is enough; if it requires uniform edge rounding and no manual traces allowed, then a form tool or a dedicated process is needed, and inspection also has to check the fillet radius. Likewise, "mating surface Ra0.4" means smaller feed, sharper tools, possibly additional finish milling or grinding, and if setup rigidity is insufficient, chatter occurs, which in turn requires lower parameters and longer machining time. None of these are main dimension changes, yet all of them enter cost.
The judgment rule is simple: any annotation that describes a "condition" rather than a "dimension" must be reduced to a measurable criterion before quoting. If it is unclear, make it clear; once it is clear, whether it can be achieved should be confirmed jointly by engineering and the factory.
| Deburr and blunt all sharp edges | Adds manual/finishing operations; edge rounding consistency is hard to control; inspection depends on appearance criteria | Deburring scope, whether manual traces are allowed, whether a radius is specified for edges |
| Mating surface Ra0.4 / Ra0.8 | Requires finish milling or grinding, lower feed, higher tool requirements, possibly additional operations | Which surfaces are mating surfaces, by what method roughness is evaluated, whether it can be relaxed |
| Unspecified tolerances per GB/T 1804-m | General profile tolerance zone is relatively wide and usually does not affect cost | Confirm the unspecified tolerance grade to avoid confusion with critical dimensions |
| Finish machining after heat treatment | Hard-state cutting or grinding, high tool wear, high setup requirements | Hardness range, sequence of heat treatment and machining |
| Surface anodizing/blackening | Adds outsourced operations and turnover; color and film thickness vary by batch | Film thickness, color sample, whether specific surfaces are masked |
The purpose of this table is not to memorize it, but to use it as a template: when you receive a drawing, first scan the annotation column and title block, and for anything that matches the table, write it item by item into the RFQ clarification checklist. Main dimensions are usually understandable at a glance; what really causes quotes to be revised back and forth are often these sentences that no one looks at carefully.
Tolerance annotation: grade by function, don't let one ±0.005 raise the cost of the whole part
The place on a drawing most likely to cost extra money is not the main dimension, but that string of tight tolerances with no functional basis. For the same aluminum part, marking the mating surface at ±0.01 mm and the remaining profile at ±0.1 mm, versus marking the entire drawing uniformly at ±0.005 mm, are two different jobs in process terms: the former can be covered with one setup and conventional toolpaths; the latter often requires additional setup datums, lower feed, finishing allowance, and inspection upgraded from calipers to CMM. A common industry practice is to annotate in three grades by function, rather than applying one uniform standard to the whole drawing.
How to divide the three tolerance bands
| Feature/Function | Common tolerance bands | Process implications | Dimensioning recommendations |
|---|---|---|---|
| Mating surfaces, locating holes, bearing seats | ±0.005–±0.02 mm | Requires control of fixturing datum and tool wear; may need fine finishing or grinding | Keep, but specify the mating counterpart and datum |
| General contours, outer profiles, steps | ±0.01–0.05 mm (typical range for standard precision CNC) | Can be covered in a single setup; within standard capability | Specify as required by assembly; no need to tighten |
| Non-functional surfaces, relief grooves, pocket floors | ±0.1–±0.3 mm or general tolerance | Not part of the fit chain; relaxing saves setups and inspection | Cover with a general tolerance note to avoid callouts at every location |
What happens if you over-tighten, and when tight tolerances can't be held anyway
Tightening non-functional surfaces to ±0.005 mm directly results in: more setups, forced conservative cutting parameters, and higher inspection frequency. Quotation differences often come from these three items, not material unit price. Conversely, even with tight callouts, thin-wall parts (wall thickness below about 0.8 mm), long overhang structures, and parts finish-machined after heat treatment may not reliably hold tight tolerance bands—distortion and residual stress eat up the margin. In such cases, confirm with the factory before quoting: relax the tolerance, change the structure, or add stress relief or split-sequence machining.
Concrete actions: First identify functional surfaces, and apply tight tolerances only to dimensions in the fit chain; use general tolerances uniformly for non-functional surfaces; call out thin walls and deep pockets separately and note the permitted process treatments. When the drawing doesn't clearly specify datums, proactively ask engineering—don't assume the factory will guess.
Thin walls, micro features, deep pockets: three features to run DFM on before quoting
Large unit price differences on quotes often aren't due to equipment cost differences, but because these three types of features weren't identified on the drawing. Common industry practice: if any one of them is present, issue a DFM report first, then quote. According to industry norms, thin walls below about 0.8 mm and feature sizes below about 2.5 mm typically require review; specific thresholds vary with material and structure, and confirmation should be based on the drawing and the factory's process judgment.
Pre-quote DFM checklist (follow in order)
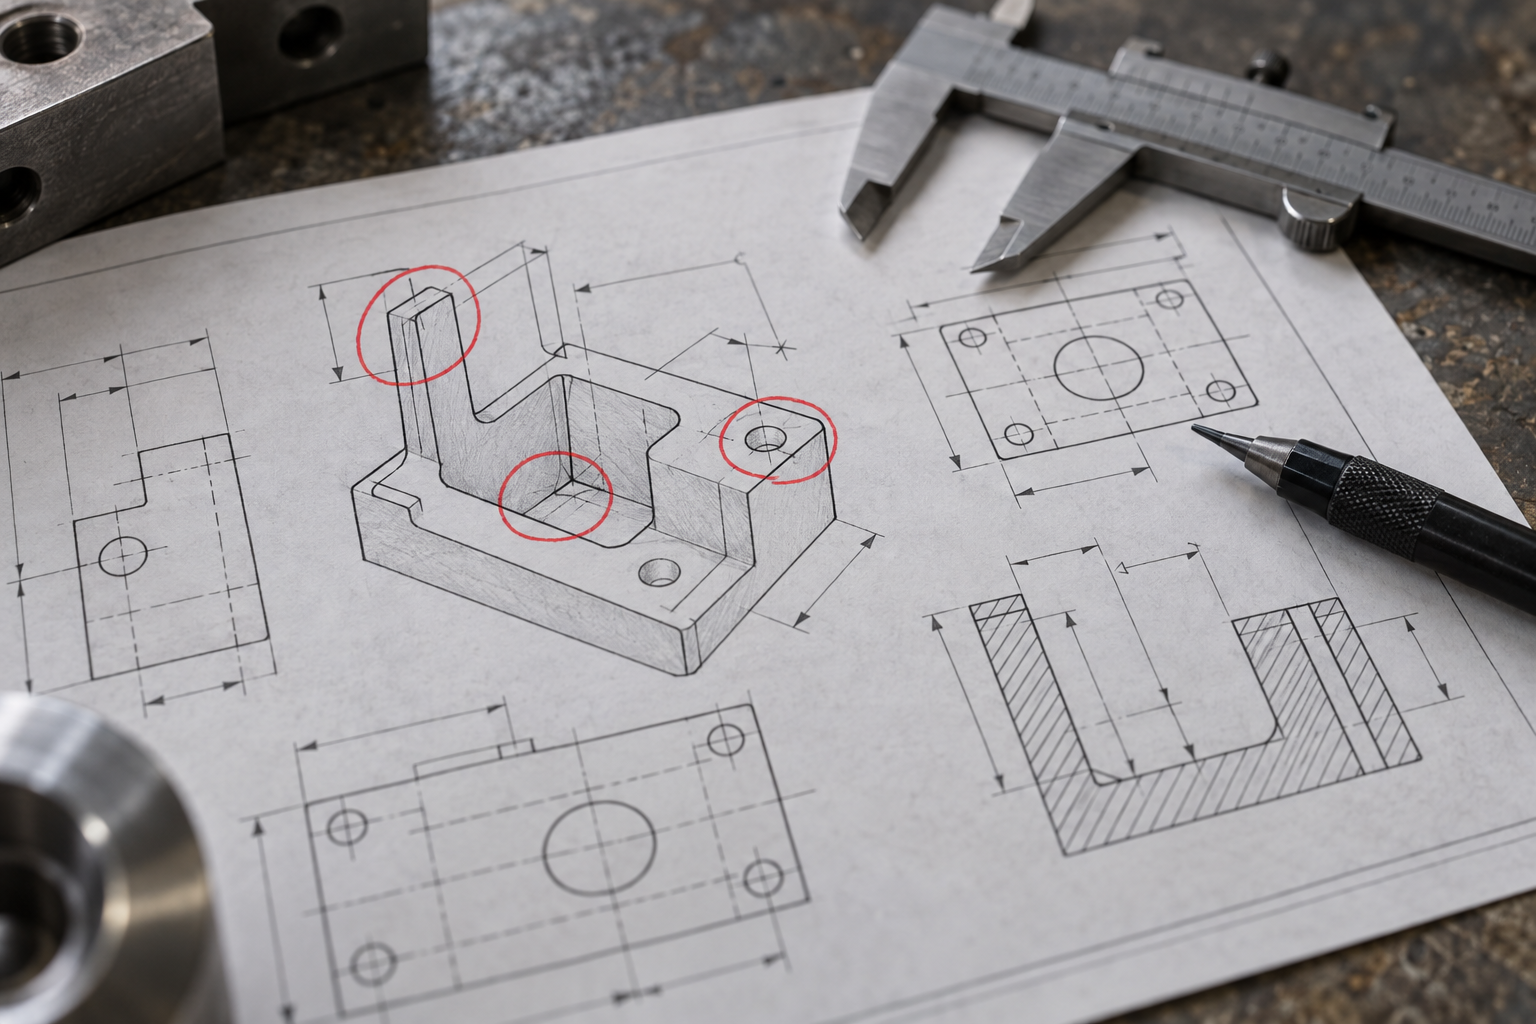
Front-loading DFM has shifted from a "quote attachment" to a "manufacturability gate": many orders decide whether to quote only after seeing the DFM conclusion. But note—DFM capability must be verifiable; don't just take their word that they can do it. You can require them to specify the tooling plan, number of setups, and inspection method in the report, rather than a one-line "no problem."
A walkthrough of a bracket part: aligning acceptance criteria from inquiry to inspection
Walking through a real automation equipment bracket drawing is more useful than ten principles. Key drawing points: two locating holes marked ±0.01, side wall thickness 0.6 mm, one pocket with a depth-to-width ratio of about 3:1, mating surface marked Ra0.8, material 6061-T6, batch of 200 pieces. Send this drawing out for quoting as-is, and the quotes that come back can differ by a factor of two—the difference lies in the number of setups and inspection criteria, not the main dimensions.
Four things to clarify before quoting
- ±0.01 locating holes: Are they for assembly locating or just a process datum? If for locating, will inspection use CMM or go/no-go gauges? Specify the hole diameter tolerance band and position tolerance separately—don't give just one dimensional tolerance.
- 0.6 mm thin wall: Clamping force during fine milling will distort it; confirm whether to leave process tabs or switch to split-sequence machining, otherwise it will spring back out of tolerance after unclamping.
- 3:1 deep pocket: A standard end mill at this length-to-diameter ratio will chatter; confirm whether the supplier has extended-length tooling or can add fillets and use stepped depth cuts.
- Ra0.8 mating surface: Is it a sealing surface or an ordinary contact surface? The former can't be relaxed; the latter can be relaxed to Ra1.6 or even Ra3.2, saving one fine milling operation.
What was changed, and how setups dropped from several to several
After clarification, three callouts were changed: non-functional surface tolerance relaxed from ±0.05 to ±0.1; R2 added to deep pocket corners with tool reach direction noted; a note added to the title block: "Mating surfaces Ra0.8, all others Ra3.2, sharp edges deburred 0.3." After the changes, setups dropped from 4 to 2 (one for the front side, one for the flip side), per-piece labor time decreased, and inspection items changed from full dimensions to a critical dimension list plus first-article CMM. Inspection criteria were agreed in sync: locating holes and mating surfaces by CMM, everything else by calipers.
Acceptance and inspection criteria: if the drawing doesn't specify, rework becomes a dispute between both parties
The same hole measures φ10.012 on a CMM, passes the go end and won't enter the no-go end with a go/no-go gauge, and feels "tight" on a caliper. Three methods, three conclusions—who's right? All of them—provided the drawing specifies which one to use. If the drawing doesn't specify inspection criteria, you're leaving the verdict to luck, and once volume ramps up, it's a dispute.
How a dimension is measured determines whether it passes
Standard practice: mating holes, locating holes, datum surfaces measured by CMM or vision system, with a first-article report; threads and through holes by go/no-go gauges; batch outer diameters by caliper sampling. But switching methods for the same dimension can change results by a few microns to over ten microns—a CMM measures single-point coordinates, while a go/no-go gauge measures the virtual size, including form error. So the drawing must specify: critical dimension list + inspection method + sampling or 100% inspection. Without it, the factory inspects by its own habits and procurement verifies by its own habits; when the two numbers on the acceptance sheet don't match, who pays for the rework?
| Feature | Common method | Agree before quoting |
|---|---|---|
| Locating hole / mating hole | CMM, vision measuring machine | Whether to provide a first article report, how many points to measure |
| Thread | Go/no-go gauge | Gauge grade, sampling ratio |
| Batch outer diameter | Snap gauge / micrometer | Sample size, upper and lower acceptance limits |
| Thin-wall contour | Vision measuring machine + CMM combination | Measurement point locations, whether deformation is included |
| Roughness mating surface | Roughness tester sampling | Ra value, which locations to measure |
The pitfall buyers fall into most easily: comparing only unit price, not fixturing plans and inspection criteria. Factory A quotes 80 yuan using two setups and full CMM inspection; Factory B quotes 65 yuan using four setups and snap gauge sampling—B's unit price is lower, but all the batch consistency risk is passed on to the assembly line. The truly comparable total cost = unit price + labor hours from the number of setups + inspection labor hours + potential rework.
Pre-quote clarification checklist: one table engineering can use right away
Consolidate the scattered points from the previous sections into one table; procurement sends it to engineering, engineering returns it to the factory, and one round is enough to align. It is not a courtesy suggestion, but a tool to eliminate "quote discrepancies" and "acceptance disputes" in advance. The table below is organized by six dimensions, each stating "what happens if it is not clarified."
| Dimension | What to clarify | Consequence of not clarifying |
|---|---|---|
| Dimensions/tolerances | Which surfaces are mating surfaces and which are non-functional surfaces; whether tight tolerances can be relaxed | The entire part is quoted at the tightest tier, inflating cost; or the factory machines by experience and inspection judges it nonconforming |
| Material and condition | Grade, heat treatment/stress relief, incoming condition (plate/bar/forging) | After material substitution, hardness, machinability, and deformation all change, causing dimensional drift |
| Surfaces and notes | Specific surfaces for roughness, deburring scope, whether anodizing/passivation/sandblasting is required | A single note may add one setup or manual finishing, changing both quote and lead time |
| Inspection method | Whether key dimensions use CMM, vision measuring machine, or snap gauge; whether a first article report is required | The same part judged differently by different measuring tools—rework responsibility becomes unclear |
| Batch size and packaging | One-off, small batch, mass production; whether anti-scratch packaging and box labeling are required | Batch consistency requirements not stated—a qualified first article doesn't mean the batch is qualified |
| Whether design changes are allowed | Whether fillets can be adjusted or walls thickened at thin walls, deep cavities, and internal sharp corners | The factory doesn't dare to change it and can only do it the hard way with multiple setups, driving up both cost and risk |
The usage is simple: procurement fills in the left two columns, engineering confirms the third column, and the factory responds item by item in the quotation. If any row says "to be confirmed," the quote should be treated as an estimate, not a committed price.
Common questions
The following are the questions most often asked and most easily answered incorrectly during the inquiry stage. The answers contain no delivery commitments and no precision guarantees—only the judgment path and the items that need to be confirmed with engineering.
The drawing specifies ±0.005 mm—can it definitely be made?
It can't be generalized. In the industry, the common tolerance band for precision CNC is about ±0.01–0.05 mm, depending on the feature, material, and fixturing; ±0.005 mm is a tighter tier, and whether it can be consistently guaranteed depends on where the dimension is located, whether the datum is unified, whether multiple setups are needed, and whether the factory's inspection methods can reproduce it. The right approach is: state the functional requirement of that dimension clearly and let the factory evaluate and give a tolerance band it can commit to, rather than specifying it rigidly first and then demanding it be met.
Can a 0.6 mm thin wall be machined?
Thin walls below about 0.8 mm usually require a DFM review first (a common industry guideline). 0.6 mm isn't impossible, but it depends on wall height, material, whether it's unsupported, whether there are reinforcing ribs, and whether it will be deformed by clamping. It's advisable to note allowed reinforcing structures or process bosses on the drawing and accept temporary support solutions proposed by the factory. Whether it can be consistently made in the end must be verified by sampling—you can't draw a conclusion directly from the drawing.
The mating surface is specified as Ra0.4—does that add cost?
It usually affects cost, because it often means slower feed rates, finer tools, or additional finishing operations, and inspection may be upgraded from calipers to a roughness tester or vision measuring machine. First confirm whether this surface really needs Ra0.4: if it's only a cosmetic surface, Ra1.6 or Ra3.2 is often sufficient; only if it's a sealing or sliding mating surface is it worth keeping. Stating the function clearly saves more cost than simply specifying a number.
How long does a quote take? Can we make one piece for verification first?
Quoting time depends on drawing completeness and the number of clarification rounds: when information is complete and materials are standard, it's usually faster; when thin walls, deep cavities, tight tolerance stacking, or non-standard threads are involved, a DFM review is needed first and the time is longer. Single-piece verification is common practice in both CNC and 3D printing, suitable for confirming the fixturing plan and key dimensions, but a qualified single piece doesn't mean batch consistency—sampling and inspection criteria still need to be confirmed before mass production. For specific timing, please refer to the actual inquiry response.
The drawing doesn't specify an inspection method—what is acceptance based on?
This is a high-incidence point for rework disputes. The same part measured with a CMM, vision measuring machine, or calipers may give different results. At the inquiry stage, agree on: which dimensions are critical, what equipment is used to measure them, whether it's sampling or full inspection, and whether a first article report is required. For anything not written on the drawing, it's advisable to add an inspection criteria statement when the order is confirmed and have both parties sign it, to avoid each side saying something different at acceptance.
Key takeaways
- Annotate tolerances by functional grading: only mating surfaces and locating surfaces get tight tolerances, while the rest use general tolerances; otherwise, cost is priced according to the tightest one.
- When wall thickness is below about 0.8 mm and features are smaller than about 2.5 mm, conduct a DFM review before quoting; otherwise, deformation and tool breakage become rework rather than machining issues.
- For features such as deep cavities, internal sharp corners, and non-standard threads, first mark the tool-accessible direction on the drawing; if it cannot be marked, it means the design is not finalized, and the quote can only be conditional.
- Annotations such as roughness, deburring, chamfering, and post-heat-treatment machining determine inspection labor and the number of setups, and can create a greater total cost gap than unit price.
- When requesting a quote, write the inspection method for key dimensions (CMM, vision measuring machine, caliper gauge, go/no-go gauge) into the drawing or attach it as a note, to avoid inconsistent acceptance criteria.



